Overview
Introduction to PUL1235/3 CNC 3-Sides Punching Machine
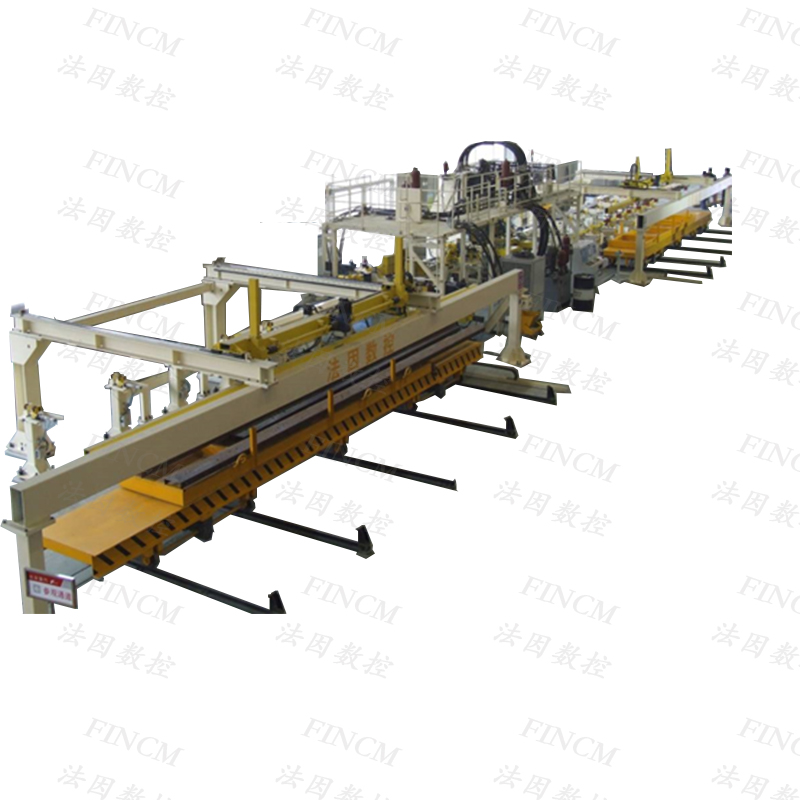
The CNC 3-sides punching machine PUL1235/3 serves as a dedicated, automated production line specifically engineered for processing truck chassis U-beams. Designed to transform raw, heavy-duty longitudinal beams into assembly-ready components, this equipment manages the entire workflow—from magnetic feeding and precise positioning to simultaneous three-sided punching and automated unloading. When standing next to the machine, operators experience the rhythmic, powerful impact of the hydraulic punches cleanly piercing thick steel plates, leaving smooth, burr-free edges. It offers commercial vehicle fabricators an industrial-grade solution that balances the demand for rapid, large-scale output with the flexibility required for specialized, small-batch frame modifications.
Core Advantages for Truck Chassis Production
Traditional U-beam processing often struggles with manual handling bottlenecks, inconsistent hole alignment, and extended setup durations. The PUL1235/3 directly resolves these operational hurdles by introducing fully synchronized automation and exact dimensional control. By minimizing manual intervention, facilities can accelerate their throughput by up to 50% while simultaneously reducing the physical strain on the workforce. The resulting efficiency makes this punching line a critical asset for heavy vehicle manufacturers aiming to scale their output without compromising on structural integrity or dimensional accuracy.
Key Features & Benefits
Full-Automatic Production Line Integration
From the initial magnetic pickup of the raw steel beam to the final automated stacking of the punched component, the entire operational cycle executes without manual lifting or positioning. This automatic punching line drastically curtails human error and ensures that the first beam of the shift matches the exact specifications of the last. For visual confirmation of this continuous workflow, we provide comprehensive video demonstrations showing the machine in action—capturing the rapid U-beam in-feed, the simultaneous three-sided high-speed punching sequence, and the controlled out-feed, allowing you to witness the raw production capacity firsthand.
High-Precision Punching & Hole Spacing Consistency
Maintaining strict tolerances is critical for vehicle safety. This machine achieves an X-direction hole spacing tolerance of ±0.3mm over 2000mm (and ±0.5mm over 12000mm), alongside a Y-direction group hole tolerance of ±0.3mm. Guided by sensitive Balluff linear sensors, the positioning remains steadfast even when handling massive 12-meter workpieces. This exceptional hole alignment directly translates to significant end-product value during final assembly. Precise hole placement ensures that chassis components align flawlessly on the assembly line, eliminating the need for forced fits or manual re-drilling, thereby enhancing the overall structural strength and assembly yield of the finished trucks.
Flexible Module Configuration for Versatile Needs
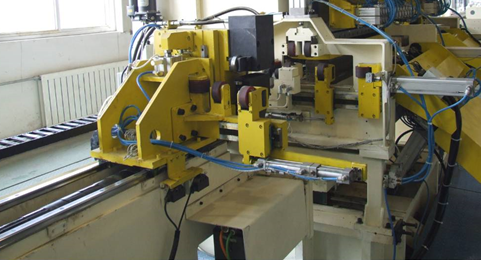
Configured with 18 movable web modules, 21 main web modules (including 5 sets of Φ25), and 6 fixed/movable flange modules, the system easily adapts to varying U-beam dimensions. It handles punching diameters ranging from the basic plate thickness up to Φ60mm on the web and Φ23mm on the flange. To further optimize operational uptime, the equipment features a quick tool change design and an automatic thin-oil lubrication system. This combination drastically reduces maintenance complexity and minimizes machine downtime during product changeovers, making it highly efficient for facilities managing multiple, distinct chassis profiles in a single day.
Exceptional Production Efficiency
Speed and power converge to maximize daily output. When processing a standard 12-meter U-beam requiring approximately 300 holes, the complete punching cycle concludes in roughly 7 minutes. Driven by rapid X and Y-axis movements reaching speeds up to 30 meters per minute, the parallel processing capabilities ensure that heavy fabrication schedules are met consistently without sacrificing dimensional integrity.
Reliable Loading & Unloading Mechanism
Handling heavy steel requires robust mechanics. The integrated magnetic feeding and downloading device utilizes 10 powerful electromagnets, each delivering 2kN of suction force, to securely grip and transfer the metal. Paired with a middle manipulator moving at 40m/min, the system guarantees smooth, vibration-free transitions of the workpieces, safely supporting finished material stacking heights up to 500mm for streamlined forklift retrieval.
Core Components & Quality Assurance
World-Class Core Components
The longevity and precision of the PUL1235/3 rely on an architecture built from globally recognized, industrial-grade parts. The operational brain is powered by the Siemens ONE CNC system and driven by responsive Siemens servo motors from Germany. Precision feedback is handled by German Balluff linear sensors, while the heavy mechanical loads glide smoothly on HIWIN linear guide rails from Taiwan, China. Pneumatic actuation is managed by reliable FESTO components. This premium component selection guarantees that the machine withstands the harsh, continuous-duty cycles typical of heavy metal fabrication environments.
Rigorous Quality Inspection Standards
Transparency in our manufacturing process is a cornerstone of our factory strength. Before any unit leaves our facility, it undergoes exhaustive process control checks, including a 100-hour continuous punching trial to verify thermal stability, hydraulic pressure consistency, and sensor accuracy under load. Our robust manufacturing capacity ensures we can fulfill large-scale fleet equipment orders strictly on schedule. This rigorous approach is validated by our extensive client cases and partnerships with globally recognized commercial vehicle and heavy-duty truck manufacturers. Their continued reliance on our machinery serves as a real-world endorsement of the equipment’s durability and our commitment to ISO-certified manufacturing standards.
Application Scenarios
Commercial Vehicle Chassis Manufacturing
Engineered specifically for processing truck chassis longitudinal beams, this machinery supports the structural foundation of light, medium, and heavy-duty commercial transport vehicles. It seamlessly accommodates the mainstream chassis designs required by major automotive brands, ensuring rapid throughput for high-demand production lines.
Automotive Longitudinal Beam Production
The system effortlessly handles the thick, high-tensile U-beams utilized in the frames of buses, lorries, and specialized utility vehicles. By maintaining strict tolerances, it meets the rigorous industry requirements for load-bearing structural components where absolute precision is non-negotiable.
Heavy-Duty Truck Frame Processing
For facilities focused on volume, this equipment serves as the ideal backbone for mass-producing heavy-duty truck frames. The consistent repeatability of hole positions ensures that subsequent assembly stages—such as riveting and bolting cross-members—proceed without alignment delays.
Custom U-Beam Component Fabrication
Beyond standard production, we offer customized CNC solutions tailored to your specific operational constraints. Whether you require adaptations for non-standard U-beam dimensions, specialized hole patterns for new vehicle prototypes, or modifications to fit a unique workshop layout, the system adapts to small-batch, multi-variety fabrication. This flexibility aggressively supports new product development cycles for forward-thinking automotive manufacturers.
Action Call & After-Sales Service
Get a Custom Quote Today
Preparing to elevate the capacity and precision of your truck chassis production facility? Inquire now to receive a detailed, tailored engineering solution and a comprehensive pricing structure. By sharing your specific U-beam dimensions, material grades, and daily output targets, our engineering team will configure the exact module setup required to maximize your operational efficiency and return on investment.
Comprehensive After-Sales Support Package
Investing in heavy machinery requires dependable, long-term backing. We deliver a complete support ecosystem, initiating with professional on-site installation and hands-on operator training to ensure your team is confident from day one. The equipment is backed by a solid 1-year warranty on all primary components, coupled with a responsive global spare parts supply network. Furthermore, our dedicated technical specialists are available for 24/7 online troubleshooting, minimizing potential disruptions and keeping your production lines moving steadily.
Data of U beam before punching | Data of U beam before punching | σb=510-890 MPa |
Length of U beam | 4000~ (+) |
Inside width of U beam web | 200-340 mm (+) |
U beam flange height | 60 (±) |
U beam thickness | 4-10 mm |
Fillet radius | R (+) |
Longitudinal straightness deviation of Web surface | 0.1%, ≤/ overall length |
Longitudinal flatness deviation of flange surface | /m, ≤/ overall length |
Maximum twist | / overall length |
Angle between flange and web | 90o±1 |
Data of U beam after punching | Punching diameter of Web | Maximum Φ 60mm. Minimum equals plate thickness |
Punching diameter of flange | Maximum Φ 23. Minimum equals plate thickness |
The minimum distance between the centerline of the hole on the web closest to the inner surface of the flange | 20mm when Hole diameter ≤ Φ 13mm 25mm when Hole diameter ≤ Φ 23 50mm when Hole diameter>Φ 23mm |
The minimum distance between the U beam inner side web surface and the centerline of flange hole | 25 mm |
The punching accuracy shall be controlled within the following range (except for the range of 200 mm at both ends) and the centerline distance accuracy between holes | Tolerance value of hole spacing in X direction: ± 0.3mm/2000mm; ±0.5mm/12000mm Tolerance value of group hole distance in Y direction:±0.3mm |
Accuracy of the Distance from hole centerline to the flange inner edge | ± |
Module position and punching travel of punching press | Movable web CNC punching press | 18 modules, straight line. |
CNC punching press for large web plate | 21 modules, straight line, 5 modules of Φ25. |
Fixed flange CNC punching press | 6 modules, straight line. |
Movable flange CNC punching machine | 6 modules, straight line. |
Punching travel of main machine |
|
Production Efficiency |
| When the length of the U beam is 12 meters and there are about 300 holes, the punching time is about 7 minutes |
Machine Overall Size | Length x Width x Height | about 36000mm x 8500mmx 4000mm. |
Loading and unloading trolley | Move travel | about 2000mm |
Move speed | about 4m/min |
Stacking height | about 500mm |
Magnetic In-feeding device / Magentic downloading device | Horizontal travel | about 2000mm |
Horizontal motor power | 1.5kW |
Vertical travel | about 600mm |
Vertical motor power | 4kW |
Number of electromagnets | 10 |
Electromagnet suction force | 2kN/each piece |
Infeeding Manipulator | Maximum speed | /min |
X-axis travel | about 3500mm |
Movable CNC Punching Press for web | Nominal force | 800kN |
Punch hole diameter types | 9 |
Module number | 18 |
X-axis travel | about 400mm |
X-axis maximum speed | 30m/min |
Y- axis travel | about 250 mm |
Y-axis maximum speed | 30m/min |
Maximum punch diameter | Φ23mm |
Main CNC Punching Press for web | Nominal force | 1700kN |
Punch hole diameter types | 13 |
Module number | 21 |
Y- axis travel | about 250mm |
Y-axis maximum speed | 30m/min |
Maximum punch diameter | Φ60mm |
Middle manipulator | Maximum speed | 40m/min |
X-axis travel | about 2000 mm |
Fixed Flange CNC punching press | Nominal force | 650kN |
Punch hole diameter types | 6 |
Module number | 6 |
Z-axis travel | about 100mm |
Z-axis maximum speed | 10 m/min |
Maximum punch diameter | Φ23mm |
Movable Flange CNC punching press | Nominal punching force | 650kN |
Punching hole diameter types | 6 |
Module number | 6 |
Y-axis travel | 160mm |
Y-axis maximum speed | 10 m/min |
Z-axis travel | about 100mm |
Z-axis maximum speed | 10 m/min |
Maximum punching diameter | Φ23mm |
Output material manipulator | Maximum speed | /min |
X axis travel | About 3500mm |
Hydraulic system | system pressure | 24MPa |
Cooling mode | Oil cooler |
Pneumatic system | working pressure | 0.6 MPa |
Electrical system |
| Siemens 840D SL |
No. | Name | Brand | Country | Remark |
1 | CNC Control System | Siemens ONE | Germany |
|
2 | Servo motor | Siemens | Germany |
|
3 | Precision linear sensor | Balluff | Germany |
|
4 | Hydraulic system | H+L | Germany |
|
5 | Other main hydraulic components | ATOS | Italy |
|
6 | linear guide rail | HIWIN | Taiwan, China |
|
7 | Wide guide rail | HPTM | China |
|
8 | Precision ball screw | I+F | Germany |
|
9 | Screw support bearing | NSK | Japan |
|
10 | Pneumatic components | SMC/FESTO | Japan / Germany |
|
11 | Single air bag cylinder | FESTO | Germany |
|
12 | Elastic coupling without backlash | KTR | Germany |
|
13 | Frequency converter | Siemens | Germany |
|
14 | computer | LENOVO | China |
|
15 | Drag chain | IGUS | Germany |
|
16 | Automatic lubrication device | HERG | Japan | Thin oil |
Note: The above is our fixed supplier. It’s subject to be replaced by same quality components of other brand if the above supplier can’t supply the components in case of any special matter.
1).Power supply: 3 phase 5 lines 380±10%V 50±1Hz
(as per Brazil local voltage)
2).Compressed air pressure: ≥0.5MPa
3).Temperature: 0
4).Humidity: ≤75%