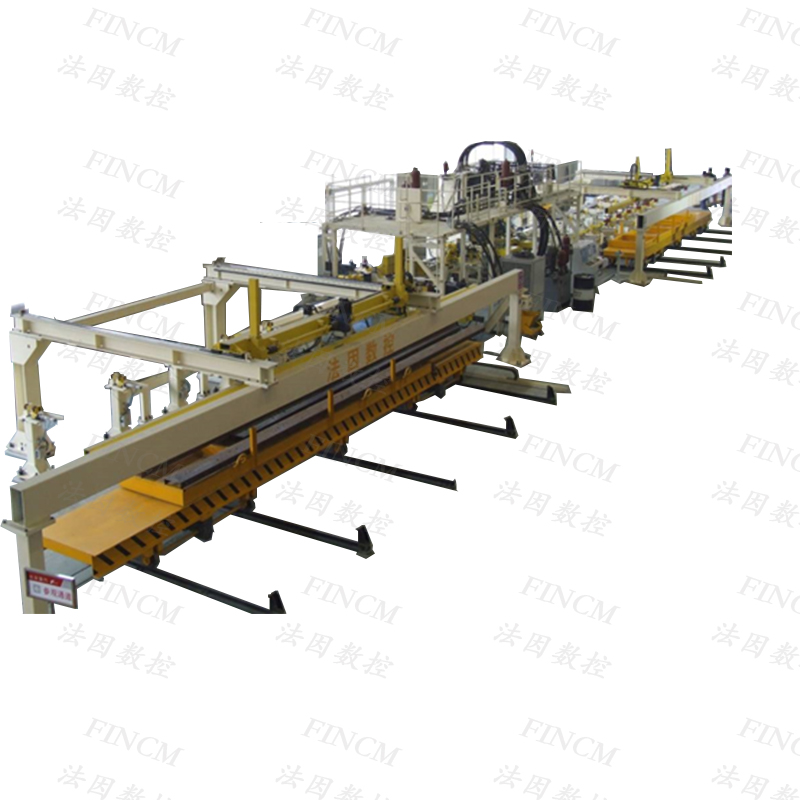
The High-Speed 3-Sides CNC Punching Machine PUL1235A/3 delivers precision processing for truck U-beams with fully automatic 3-side punching, boosting production efficiency and quality in chassis manufacturing. Its advanced CNC technology ensures high-speed, high-accuracy operations for both mass production and flexible small-batch development.
- Fully automatic 3-side punching for equal-cross-section U-beams - High processing precision with Siemens 840D SL CNC system - Fast punching speed and optimized production efficiency - Adaptable for mass production and small-batch new product development
Engineered specifically for heavy-duty truck chassis manufacturing, the CNC 3-Sides Punching Machine PUL1235A/3 transforms raw U-beams into precision-punched frame components. This industrial powerhouse integrates advanced numerical control with a rigid mechanical architecture to execute simultaneous three-sided piercing. By automating the handling and processing of equal-cross-section U-beams, it drastically reduces production preparation time. Operators on the factory floor will immediately notice the smooth, vibration-free operation and the distinct, rhythmic sound of efficient metal piercing as the machine effortlessly handles both high-volume longitudinal beam runs and small-batch prototype developments. Every structural detail is optimized to improve the overall assembly precision and operational efficiency of commercial vehicle manufacturing.
Key Features & Benefits
Full-Automatic 3-Side Punching System
The equipment features strategically positioned movable and fixed CNC punching units dedicated to the web and flanges. This configuration allows simultaneous three-sided piercing without requiring operators to manually reposition heavy steel beams. By replacing multi-step manual handling with a continuous automated workflow, facilities can significantly reduce labor dependencies and accelerate their return on investment. This streamlined process maximizes material utilization and slashes operational overhead, turning a traditionally labor-intensive task into a highly cost-effective operation.
Exceptional Processing Precision
Driven by the sophisticated Siemens 840D SL CNC system, this machinery delivers ultra-precise positioning that production managers can rely on. The X-axis hole spacing tolerance is tightly maintained at ±0.3mm per 2000mm (and ±0.5mm over 12000mm), while the Y-axis group hole distance tolerance stays within ±0.3mm. This meticulous accuracy ensures that every U-beam aligns perfectly during final truck chassis assembly, eliminating the frustration and extra costs associated with manual rework or forced adjustments on the assembly line.
High-Speed Punching Performance
Time is a critical metric in automotive manufacturing, and this unit excels with a maximum X/Y axis travel speed of 30 meters per minute. When processing a standard 12-meter U-beam requiring approximately 300 holes, the entire cycle is completed in merely 5.5 minutes. You can hear the rapid, consistent thud of the hydraulic punch as it systematically works down the beam, easily keeping pace with the most demanding production schedules and tight delivery windows.
Flexible Production Compatibility
Built to handle diverse structural requirements, the system accommodates U-beams exceeding 4000mm in length, with web inner widths ranging from 150 to 340mm and material thicknesses between 4 and 10mm. It utilizes 18 linear modules for web operations and 6 for flange tasks, supporting over 9 different punch diameters. Equipped with a rapid tooling changeover system, operators can smoothly transition between different product specifications, making it an ideal asset for multi-variety, small-batch orders and new product development.
Intelligent Material Handling
Heavy steel beams are moved effortlessly via magnetic in-feeding and out-feeding devices, supported by heavy-duty loading trolleys and feeding manipulators. Ten powerful electromagnets, each generating 2kN of suction force, securely grip the metal, preventing any slippage during transit. The trolley moves at a steady 4m/min and supports a stacking height of 500mm, ensuring that material flow remains uninterrupted, safe, and highly organized throughout the shift.
Software Integration & Programming
To further reduce the technical barrier for floor operators, the system directly interfaces with mainstream CAD/CAM software. Production engineers can utilize one-click graphical imports to generate automated machining programs instantly. This digital handshake minimizes manual data entry errors and ensures that complex hole patterns are translated perfectly from the digital blueprint to the physical steel, optimizing the entire pre-production phase.
Core Components & Quality Assurance
Premium Core Components
Reliability starts with the internal architecture. This machine is constructed using globally sourced, premium-grade components designed for heavy industrial use. The control and motion are driven by the Siemens 840D SL CNC system and servo motors from Germany. Precision is guaranteed by Balluff linear sensors, while the heavy lifting is managed by a German H+L hydraulic system. Smooth linear motion is facilitated by HIWIN guide rails from Taiwan, China, supported by Japanese NSK screw bearings and SMC/FESTO pneumatic elements. The tactile feel and solid assembly of these industrial-grade parts underscore a commitment to longevity and stable, uninterrupted operation.
Strict Quality Control & Smart Maintenance
Every PUL1235A/3 chassis punching unit undergoes exhaustive testing against stringent international industrial standards before reaching the shipping dock. The heavy, vibration-dampening frame ensures a low failure rate even under continuous, high-load shifts. Furthermore, the advanced Siemens control system provides real-time monitoring and smart diagnostic alerts. By tracking machine health and utilizing predictive maintenance protocols, facility managers can prevent unexpected downtime. The integration of energy-efficient hydraulic systems and comprehensive physical safety guards protects both the operators and your operational budget.
Application Scenarios
Primary Application
Truck/Lorry Chassis Manufacturing: The primary domain for this machinery is the demanding environment of heavy-duty and light commercial truck chassis manufacturing. It serves as the backbone for producing the critical structural U-beams that form the automobile frame. Leading commercial vehicle manufacturers have integrated this exact model into their active production lines, providing documented video proof of its exceptional stability and precision during continuous, multi-shift operations.
Extended Uses
Special Vehicle Customization: Beyond standard trucks, the equipment offers modular customization to suit the unique structural requirements of special utility vehicles, engineering trucks, refrigerated transports, and logistics fleets.
Automobile Parts Suppliers: For auto parts suppliers managing diverse client portfolios, the machine's scalable design allows for fluid integration into existing automated chassis production lines. It provides the exact flexibility needed to tackle complex, non-standard U-beam dimensions without requiring a complete factory overhaul.
Action Call & After-Sales Service
Ready to upgrade your truck chassis U-beam processing line? Inquire now for a custom quote or Add to Basket to secure your machine! Investing in the PUL1235A/3 means upgrading your entire structural processing capability. Our dedicated engineering support team stands ready to assist you with a comprehensive service package designed to maximize your operational uptime:
• On-site installation and commissioning by certified technicians to ensure perfect calibration.
• Free, hands-on operation and maintenance training for your staff to build internal expertise.
• Global supply of genuine spare parts with fast delivery to keep your lines moving.
• 24/7 remote technical support to resolve issues promptly and prevent unexpected delays.
• 1-year warranty and lifelong maintenance services to ensure continuous, profitable production.
Data of U beam before punching
Data of U beam before punching
σb=510-890 MPa
Length of U beam
4000~ (+)
Inside width of U beam web
150-340 mm (+)
U beam flange height
60 (±)
U beam thickness
4-10 mm
Fillet radius
R (+)
Longitudinal straightness deviation of Web surface
0.1%, ≤/ overall length
Longitudinal flatness deviation of flange surface
/m, ≤/ overall length
Maximum twist
/ overall length
Angle between flange and web
90o±1
Data of U beam after punching
Punching diameter of Web
Maximum Φ 65mm.
Minimum equals plate thickness
Punching diameter of flange
Maximum Φ 21.
Minimum equals plate thickness
The minimum distance between the centerline of the hole on the web closest to the inner surface of the flange
20mm when Hole diameter ≤ Φ 13mm
25mm when Hole diameter ≤ Φ 23
50mm when Hole diameter>Φ 23mm
The minimum distance between the U beam inner side web surface and the centerline of flange hole
25 mm
The punching accuracy shall be controlled within the following range (except for the range of 200 mm at both ends) and the centerline distance accuracy between holes
Tolerance value of hole spacing in X direction: ± 0.3mm/2000mm; ±0.5mm/12000mm
Tolerance value of group hole distance in Y direction:±0.3mm
Accuracy of the Distance from hole centerline to the flange inner edge
±
Module position and punching travel of punching press
Numerical control punching machine for movable web plate
18 modules, straight line.
CNC punching press for small web plate
18 modules, straight line, 5 modules of Φ25.
Fixed wing plate CNC punch
6 modules, straight line.
Movable flange CNC punching machine
6 modules, straight line.
Punching travel of main machine
Production Efficiency
When the length of the U beam is 12 meters and there are about 300 holes, the punching time is about 5.5 minutes
Machine Overall Size
Length x Width x Height
about 37000mm x 8500mmx 4000mm.
Loading and unloading trolley
Move travel
about 2000mm
Move speed
about 4m/min
Stacking height
about 500mm
Magnetic In-feeding device /
Magentic downloading device
Horizontal travel
about 2000mm
Horizontal motor power
0.75kW
Vertical travel
about 600mm
Vertical motor power
2.2kW
Number of electromagnets
10
Electromagnet suction force
2kN/each piece
Infeeding Manipulator
Maximum speed
/min
X-axis travel
about 3500mm
Movable CNC Punching Press for web
Nominal force
800kN
Punch hole diameter types
9
Module number
18
X-axis travel
about 400mm
X-axis maximum speed
30m/min
Y- axis travel
about 250 mm
Y-axis maximum speed
30m/min
Maximum punch diameter
Φ23mm
CNC Punching Press for small web plate
Nominal force
800kn
Punch type
9
Module number
18
Y-axis stroke
About 250mm
Maximum speed of y-axis
30 m/min
Maximum punch diameter
Φ23 mm
Main CNC Punching Press for web
Nominal force
20000kN
Punch hole diameter types
10
Module number
10
Y- axis travel
about 250mm
Y-axis maximum speed
30m/min
Maximum punch diameter
Φ65mm
Middle manipulator
Maximum speed
40m/min
X-axis travel
about 2000 mm
Fixed Flange CNC Punching Press
Nominal force
650kN
Punch hole diameter types
6
Module number
6
Z-axis travel
about 100mm
Z-axis maximum speed
10 m/min
Maximum punch diameter
Φ23mm
Movable Flange CNC Punching Press
Nominal punching force
650kN
Punching hole diameter types
6
Module number
6
Y-axis travel
160mm
Y-axis maximum speed
10 m/min
Z-axis travel
about 100mm
Z-axis maximum speed
10 m/min
Maximum punching diameter
Φ23mm
Output material manipulator
Maximum speed
/min
X axis travel
About 3500mm
Magnetic downloading device
Horizontal movement travel
About 2000mm
Horizontal movement motor power
0.75kw
Vertical movement travel
About 600mm
Vertical movement motor power
2.2kw
Electromagnetic Numbers
10
Electromagnetic Sucking Force
2kN/ each
Hydraulic system
system pressure
24MPa
Cooling mode
Oil cooler
Pneumatic system
working pressure
0.6 MPa
Electrical system
Siemens 840D SL
No.
Name
Brand
Country
Remark
1
CNC
Siemens 840D SL
Germany
2
Servo motor
Siemens
Germany
3
Precision linear sensor
Balluff
Germany
4
Hydraulic system
H+L
Germany
5
Other main hydraulic components
ATOS
Italy
6
linear guide rail
HIWIN
Taiwan, China
7
Wide guide rail
HPTM
China
8
Precision ball screw
I+F
Germany
9
Screw support bearing
NSK
Japan
10
Pneumatic components
SMC/FESTO
Japan / Germany
11
Single air bag cylinder
FESTO
Germany
12
Elastic coupling without backlash
KTR
Germany
13
Frequency converter
Siemens
Germany
14
computer
LENOVO
China
15
Drag chain
IGUS
Germany
16
Automatic lubrication device
HERG
Japan
Thin oil
1).Power supply: 3 phase 5 lines 380±10%V 50±1Hz (as per Brazil local voltage)