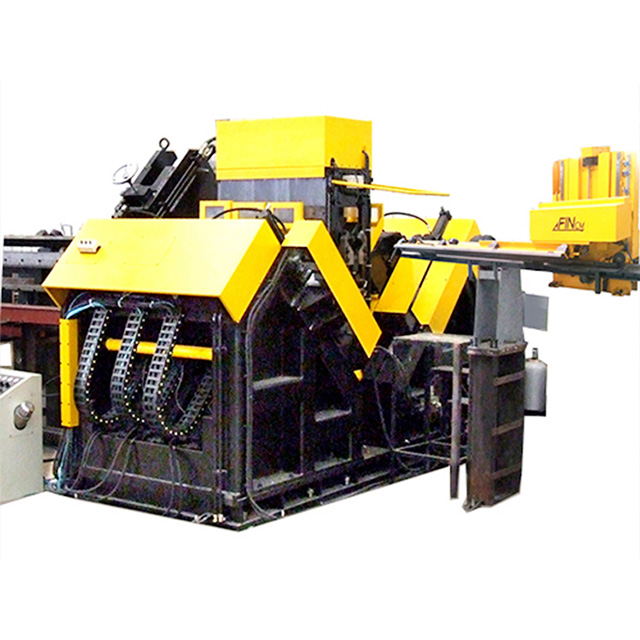
250x250mm CNC Angle Drilling Marking Machine for Tower
The BL2532 CNC Angle Drilling Marking Machine delivers precision large-angle steel processing for transmission towers, communication structures, and industrial frameworks. Combining multi-spindle drilling with permanent marking, it boosts efficiency by 40% while ensuring ±0.03mm accuracy and full traceability.
- Processes angle steel from 140×140×10mm to 250×250×32mm with 3 independent spindles (60% faster than single-spindle machines) - ±0.03mm drilling accuracy with variable speed control (180-560 rpm) for φ10mm-φ40mm holes - Integrated 1030kN marking system for permanent part numbering and batch coding - 7.5kW motor power per spindle, optimized for heavy structural fabrication
The BL2532 CNC Angle Drilling Marking Machine serves as a primary processing center for heavy-duty angle steel, specifically engineered for transmission towers, large-scale communication arrays, and wind turbine support frameworks. Capable of handling substantial angle steel dimensions ranging from 140×140×10mm up to 250×250×32mm, this equipment fundamentally transforms workshop throughput. By integrating multi-spindle drilling operations with permanent physical marking in a single automated pass, facilities can reduce their total production time by up to 40% to 60% compared to utilizing separate, isolated machines. The financial return on investment becomes apparent quickly through drastic reductions in manual material handling, lower labor overhead, and faster project turnarounds. Key performance metrics include a verified ±0.03mm drilling precision and a formidable 1030kN marking force, ensuring deep, legible traceability on every single structural component that leaves your factory floor.
Product Features
Multi-Spindle Drilling Efficiency
The equipment incorporates 3 independent drilling spindles positioned on each side, allowing for the simultaneous creation of multiple holes during a single material pass. Driven by dedicated 7.5 kW motors, each spindle offers variable speed adjustments ranging from 180 to 560 rpm, easily accommodating drill bit diameters between φ10mm and φ40mm. This specific multi-spindle architecture is a direct catalyst for operational efficiency, slashing processing times by up to 60% when compared to conventional single-spindle alternatives processing complex hole patterns. By minimizing the need for constant tool changes and repeated material indexing, production managers can significantly lower labor intervention and material flow costs. The accelerated throughput translates directly into a shortened equipment payback period, maximizing the economic yield of your structural fabrication line.
Integrated Marking System
A specialized marking station applies a nominal stamping force of 1030 kN, executing permanent indentations of batch codes, part numbers, and quality identifiers directly into the raw steel surface. You can physically run your fingers over the deep, crisp indentations left on the metal, ensuring long-term readability even after heavy galvanization or decades of outdoor weathering. The marking head utilizes interchangeable character dies, and the system fully supports the development of exclusive character molds tailored to specific regional or corporate requirements. By consolidating the marking and drilling phases, facilities eliminate secondary labeling tasks. This comprehensive approach guarantees strict component traceability across the entire supply chain, while the system's adaptable nature allows it to integrate flawlessly with existing heavy tower processing workflows.
Large Angle Capacity & Safety Standards
Living up to its industrial designation, the BL2532 confidently processes medium to massive angle steel sections spanning from 140×140×10mm up to 250×250×32mm. The material feeding mechanism relies on servo-driven rollers equipped with adjustable pressure configurations, maintaining a firm grip on the heavy steel without causing surface deformation or compromising positional accuracy. Beyond its physical capacity, the entire machine architecture adheres to strict CE and ISO international industrial safety standards. The work zone is fortified with comprehensive overload protection circuits, strategically placed emergency stop mechanisms, and heavy-duty protective enclosures. These physical safeguards protect operators from flying metal chips and moving mechanical components, ensuring a secure workshop environment during continuous, high-volume production shifts.
Advanced CNC Control & Core Components
At the brain of the operation is an industrial-grade CNC interface featuring a responsive 12-inch touchscreen display. The software environment supports direct CAD file imports and offline programming, enabling operators to visualize 3D simulations of the drilling and marking paths prior to actual material engagement. This preview capability drastically reduces setup times and prevents costly raw material waste, storing up to 1000 processing programs for complex tower components. To ensure extreme reliability under punishing daily usage, the system is built upon a foundation of premium international components, including Panasonic servo motors, ATOS hydraulic valves, and HIWIN linear guides. Furthermore, the electrical architecture can be customized to match specific national industrial voltage requirements, ensuring immediate compatibility upon delivery to any global manufacturing facility.
Applications
High-Voltage Transmission Towers
The BL2532 is heavily utilized in the fabrication of structural components for 220kV and 500kV electrical transmission towers. It excels at drilling exact connection points across tower legs, crossarms, and diagonal bracing members. Because these towering structures face immense environmental stresses, the structural integrity of every bolted joint is non-negotiable. The machine's strict adherence to precision ensures that field assembly crews experience perfect hole alignment, eliminating the need for dangerous and time-consuming manual re-drilling on site. Concurrently, the integrated marking guarantees that every individual steel member retains its specific identification code throughout the manufacturing process and final installation.
Heavy-Duty Communication Towers
When constructing telecommunication arrays that exceed 50 meters in height, the underlying load-bearing structures demand thick-walled, heavy-gauge angle steel. This CNC equipment processes these dense materials with consistent power, delivering the exact hole geometries required for critical structural joints and heavy antenna mounting brackets. Operators can hear the rhythmic, controlled hum of the servo motors as the heavy steel is fed through the machine, reflecting the controlled power applied to each operation. The resulting precision guarantees that the assembled communication towers maintain their vertical plumb and structural rigidity under extreme wind loads.
Wind Turbine Support Structures
Within the renewable energy sector, the demand for massive, perfectly engineered support frameworks is constant. This machine handles the rigorous drilling and marking of angle steel components utilized in wind turbine lattice towers and foundational anchoring systems. In these applications, the exact mathematical positioning of every drill hole is critical for the even distribution of dynamic loads generated by the rotating turbine blades. The equipment's rigid linear guides prevent lateral deflection during the heavy drilling process, ensuring that the final steel lattice can safely absorb and transfer immense kinetic forces.
Bridge and Industrial Structures
Moving beyond vertical tower construction, the BL2532 proves equally valuable in the civil engineering and heavy industrial sectors. It routinely processes large-scale angle steel used for bridge cross-bracing, overhead crane runways, and offshore oil platform support members. These heavy-duty structural applications require materials that can withstand punishing weight and continuous vibration. The machine's ability to maintain tight dimensional tolerances across long lengths of thick steel ensures that bridge and platform fabricators can meet strict engineering codes, accelerating large-scale construction schedules.
FAQ
What is the drilling accuracy of the BL2532?
The equipment consistently achieves a positional accuracy of ±0.03mm for all drilled holes, ensuring perfect alignment across hundreds of identical structural components. Before any unit leaves our manufacturing facility, it undergoes a rigorous quality control regimen, including strict laser interferometer precision calibration and actual raw material test runs. This physical verification ensures that the stated accuracy and the marking force perform exactly as specified under real-world conditions, easily satisfying the stringent engineering tolerances mandated for high-load structural connections.
How fast can the machine drill a standard hole?
When processing a standard φ25mm hole through 20mm thick Q345 industrial angle steel, the equipment completes a full drilling cycle in approximately 12 seconds per hole. However, the true speed advantage is realized through the multi-spindle architecture. By engaging multiple spindles simultaneously on different faces of the steel, the overall throughput multiplies proportionally with the number of holes per pass. This simultaneous processing capability drastically reduces the total time the material spends inside the machine, clearing production backlogs faster.
What types of marking can be applied?
The integrated stamping station is configured to apply alphanumeric characters up to 12mm in height, alongside basic geometric logos and specific quality control identifiers. The physical depth of the impression can be finely adjusted between 0.1mm and 0.5mm, depending entirely on the thickness of the raw material and the specific traceability demands of the project. We also offer the development of custom character molds, allowing facilities to imprint proprietary corporate symbols directly into the metal.
Can the machine handle pre-painted or coated angle steel?
Yes, the equipment is fully capable of processing pre-painted or protective-coated angle steel without degrading the surface finish. By utilizing specialized drill bits and carefully adjusting the variable feed rates, operators can achieve clean penetrations without causing the surrounding paint to chip or burn. Additionally, the hydraulic marking system can be dialed back to apply a lighter, more controlled force. This precise adjustment prevents the protective coating from flaking off around the stamped characters while maintaining visibility.
What maintenance is required for optimal performance?
Routine upkeep involves daily checks of the coolant reservoir and automated chip removal conveyors, weekly greasing of the linear guides and ball screws, and monthly verification of the spindle alignments. The intelligent CNC interface actively tracks tool usage, issuing predictive warnings to replace drill bits after 500–800 holes, depending on the steel's hardness. To support your long-term operations, we provide a comprehensive global after-sales network, including on-site installation, software training, lifetime technical guidance, and a rapid-response supply chain for original factory spare parts.
Packaging & Global Logistics
Transporting a heavy-duty, 12-meter industrial machine across oceans requires meticulous preparation and specialized handling. To guarantee that the equipment arrives at your facility in pristine condition, we implement a rigorous export packaging protocol:
Moisture-Barrier Vacuum Sealing: The entire central machine body and sensitive electronic control cabinets are completely enclosed in heavy-duty vacuum packaging, effectively preventing any rust or oxidation during extended maritime transit.
Structural Container Reinforcement: The equipment is secured within the shipping containers using engineered wooden blocking and heavy-duty steel tension strapping, preventing shifting during rough sea conditions.
Component Organization: All interchangeable character dies, spare servo motors, and linear guide components are individually boxed and cataloged for immediate identification upon uncrating.
Unloading Guidance: Each shipment includes detailed, step-by-step rigging and lifting schematics, ensuring your local crane operators can safely extract the heavy machinery from the container without applying stress to sensitive structural points.
CNC Drilling and Marking Machine for Angles
Machine Model: BL2532
CNC angle steel drilling machine BL2532 is mainly used for drilling and stamping of large size and high strength angle steel in transmission line tower. All the holes on the angle steel can be drilled in the production line, with high quality and position accuracy, high production efficiency and automation.
1)Technical specification of BL2532
Angle size(mm)
140×140×10 ~ 250×250×32
Range of Back mark value(mm)
50 ~ 220( stepless)
The quantity of drilling cow per side
arbitrariness
Quantity of drilling spindle per side
3
Range of drilling diameter
(H.S.S twist drill)(mm)
φ17.5 ~ φ40mm
Motor power of drilling spindle (KW)
2×5.5
Rotation speed of spindle(r/min)
180 -560(stepless adjustment)
Feeding speed(mm/min)
20 ~ 280
Quantity of CNC axis
3
Max.length of workpiece (m)
12m
Angle feeding speed (m/min)
40
Marking force (kN)
1030
Marking character Nos. (pcs)
18
Marking character Dimension (mm)
14x10x19 (LxWxH)
Quantity of character group
1 group
The max length of finished angle
12m
Hydraulic Power Pack’s cooling way
By air cooling
2) List of accessories and spare parts of BL2532
Serial
No.
Code
Name
quantity
remark
1
BL20.2-73
The upper claw
2
Including claw installed in the machine
2
BL20.2-73A
The upper claw
2
3
BL20.2-73B
The upper claw
2
4
BL20.2-74
The nether claw
2
Including claw installed in the machine
5
BL20.4-12
character
10
Character 0 to 9
6
MT.4-MT.3
reducing sleeve (length 157)
2
including the reducing sleeve installed in the machine
7
MT.4-MT.3
reducing sleeve (length 202)
2
including the reducing sleeve installed in the machine
8
MT.4-MT.3
reducing sleeve (length 247)
2
including the reducing sleeve installed in the machine
9
MT.4-MT.2
reducing sleeve
(length 178.5)
4
including the reducing sleeve installed in the machine
10
MT.4-MT.2
reducing sleeve
(length 223.5)
4
including the reducing sleeve installed in the machine
11
MT.4-MT.2
reducing sleeve
(length 268.5)
4
including the reducing sleeve installed in the machine
12
SHZ14A-2
Spring
2
13
BL20.2-77
Extention spring
2
14
4×90×50
Timing belt
1
15
Air gun
1
16
Common tools(including:full set of inner hexangular wrench, 500, 300, 150MM adjustable wrench, two solid wrench, a set of screwdriver)
1set
17
Pressure oiler
1
18
Drawing of wearing parts
2
19
Quality Certificate,Packing List
1 volume each
20
Instruction(mechanical part)
Instruction(electric part)
2 volume
each
3) List of the Key Outsourced Components of BL2532